Introduction
Every food manufacturer intends to implement the best possible food safety and quality assurance systems and adopt a stance of continuous improvement. The particular ways you achieve that will depend on a massive range of variables – depending on your process and the nature of the materials you handle. There is no one size fits all approach, so professionals and management teams should optimise for problem-solving and ongoing improvement in order to adapt to technological, legal, supply-chain developments.
In this post, we’ll look at a few methodologies that you can apply to situations you encounter – so that you have a framework for proactive improvements and deviations-handling.
As we dive into the topic, you’ll be interested to know that Food Industry Hub offers integrated management systems for food manufacturers, which you can use to strengthen your assurance processes.
Table of Contents
Voluntary Assurance Schemes
While voluntary assurance schemes don’t directly serve continuous improvement or problem-solving, they can present a very useful framework for the development of assurance systems. If you model assurance systems around the requirements of GSFI-recognised assurance schemes, you’ll have given consideration to a wide range of assurance processes that you may have otherwise overlooked.
It’s important to acknowledge that compliance to a voluntary assurance scheme is not, by itself, a guarantee of a well-implemented quality system. Auditable schemes define outcomes that your quality management system must achieve in order to be found compliant, and these outcomes can be achieved in many different ways.
If you look at scheme requirements as guidance for identifying processes, systems, and risk factors that need to be accommodated for by your food safety and quality assurance system, you can integrate those key considerations into the systems you implement. On the other hand, it can be erroneous/dangerous if you make the assumption that your site has robust quality assurance processes by virtue of the fact that you passed an audit.
Voluntary assurance schemes like BRCGS (Brand Reputation through Compliance), FSSC 22000 (Food Safety System Certification), and IFS (International Featured Standards) can be really constructive in enhancing food manufacturers’ assurance systems. These schemes provide a framework and guidelines for improving food safety, quality, and overall assurance. Here’s how these schemes can be used to enhance assurance systems in food manufacturing:
Structured Framework for Compliance: Voluntary assurance schemes offer a structured framework that outlines the requirements and expectations for food safety and quality. Manufacturers can use these frameworks as a guide to ensure they meet industry standards.
Risk Assessment and Management: These schemes often emphasise risk assessment and management as a fundamental aspect of their requirements. Manufacturers can use these standards to identify potential risks in their processes and supply chain and develop strategies to mitigate them effectively.
Consistency and Standardisation: BRCGS, FSSC 22000, and IFS promote consistency and standardisation in processes and procedures. Manufacturers can use these standards to ensure that their products meet the same quality and safety specifications consistently. This is permissive of approval for supply between buyer and seller.
Continuous Improvement: GSFI recognised schemes encourage a culture of continuous improvement. Manufacturers are required to regularly review and update their processes and procedures to meet changing industry standards and best practices. This commitment to improvement can lead to enhanced assurance systems.
Supplier Management: Assurance schemes include requirements for supplier management and traceability. Manufacturers can use these guidelines to strengthen their relationships with suppliers and ensure the quality and safety of raw materials and ingredients.
Training and Employee Competency: Auditable schemes require employees to undergo training and maintain competency in food safety and quality processes. Manufacturers can invest in training programs that align with these requirements to ensure that their workforce is well-equipped to uphold food safety and quality standards.
Transparency and Documentation: Assurance schemes emphasise the importance of documentation and record-keeping. Manufacturers can use these requirements to create a robust system for documenting all processes, procedures, and quality control measures, promoting transparency and accountability.
Auditing and Certification: Seeking certification under these schemes involves rigorous auditing processes. Manufacturers can use these audits as an opportunity to identify areas for improvement and corrective actions to enhance their assurance systems.
Market Access and Competitive Advantage: Certification under these schemes can open doors to new markets and customers, providing a competitive advantage. Manufacturers can leverage these certifications to demonstrate their commitment to quality and safety to potential partners and consumers – as well as meeting internal quality and safety objectives.
Voluntary assurance schemes like BRCGS, FSSC 22000, and IFS offer valuable tools and guidelines for food manufacturers to improve their assurance systems. By embracing these schemes, manufacturers can not only meet industry standards but also enhance their processes, reduce risks, and build a reputation for producing safe and high-quality food products.
Plan Do Check Act for Food Safety and Quality Assurance Improvement
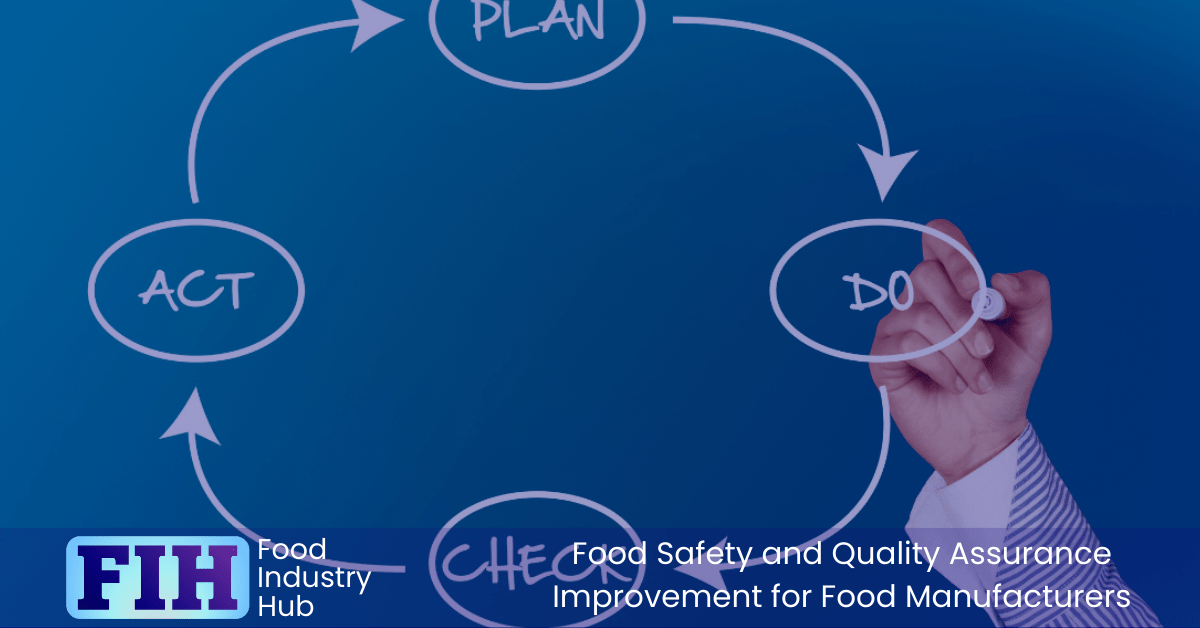
The Plan-Do-Check-Act (PDCA) cycle is a powerful approach that can be harnessed to continuously enhance food safety and quality assurance.
Understanding the PDCA Approach
The PDCA cycle, often referred to as the Deming Cycle or Shewhart Cycle, is a four-step management methodology developed by Dr. W. Edwards Deming. It is designed to facilitate continuous improvement in processes, products, and services. Let’s delve into how each step of the PDCA cycle can be tailored to food safety and quality assurance:
1. Plan
The first step, “Plan,” involves meticulous planning to ensure food safety and quality:
Identify Risks: Begin by identifying potential risks in the food production process, from ingredient sourcing to final packaging.
Set Objectives: Define clear, measurable objectives for food safety and quality standards. These objectives should align with regulatory requirements and consumer expectations.
Develop a Plan: Create a comprehensive plan that outlines the steps, procedures, and strategies needed to achieve these objectives. Ensure that everyone involved understands their roles and responsibilities.
Risk Assessment: Conduct a thorough risk assessment to anticipate potential issues and devise strategies to mitigate them.
2. Do
The “Do” phase involves executing the plan:
Implement the Plan: Put the plan into action as per the guidelines established during the planning phase.
Data Collection: Continuously collect data and information throughout the production process. This includes monitoring temperature, sanitation procedures, and product quality.
Real-Time Adjustments: Be prepared to make necessary adjustments in real-time to address any issues that arise during production.
Employee Training: Ensure that all employees are well-trained in food safety protocols and quality assurance measures and that they follow these protocols diligently. Each managerial intervention should be accompanied by training for implementation.
3. Check
In the “Check” phase, the focus shifts to evaluation and analysis:
Data Analysis: Analyse the data collected during production. Compare the actual outcomes with the predetermined objectives and standards.
Deviation Identification: Identify any deviations or variances from the desired food safety and quality parameters.
Root Cause Analysis: Determine the root causes of any issues or discrepancies. Isolate the factors that contributed to problems in the production process.
Audit and Inspection: Regularly conduct internal audits and inspections to ensure compliance with standards.
4. Act
The “Act” phase involves taking action based on the findings from the “Check” phase:
Corrective Actions: Implement corrective actions to address the issues identified during the evaluation. These actions could include process changes, additional training, or equipment upgrades.
Process Improvement: Make necessary adjustments to the plan, processes, or procedures to prevent similar issues in the future.
Standardisation:Ensure that successful changes are standardised, becoming integral parts of the new process.
Prepare for the Next Cycle: Prepare for the next iteration of the PDCA cycle by considering lessons learned from the previous cycle and setting new objectives for improvement.
Benefits of the PDCA Approach in Food Safety and Quality Assurance
Continuous Improvement: The PDCA cycle fosters a culture of ongoing learning and improvement, allowing food manufacturers to adapt to evolving challenges and regulations.
Proactive Problem-Solving: It provides a systematic approach to identifying and addressing issues, enabling early intervention and risk mitigation.
Data-Driven Decisions: Data collection and analysis lead to informed, evidence-based decisions, reducing the reliance on guesswork.
Efficiency and Consistency: Continuous improvement efforts lead to more streamlined and efficient processes, ensuring consistency in product quality and safety.
Compliance and Consumer Trust: Regular audits and proactive measures demonstrate a commitment to compliance and food safety, earning consumer trust and loyalty.
The Plan-Do-Check-Act (PDCA) cycle can be a really useful tool for achieving continuous improvement. By systematically applying this approach, food manufacturers can not only meet regulatory standards but also exceed consumer expectations, build trust in their brands, and ensure that every meal served is safe and of the highest quality. Embrace the PDCA cycle as your guide to excellence in food safety and quality assurance, and watch your products shine in the marketplace.
Sign up for the Food Industry Hub Mail Service
Receive Food Industry Hub updates, resources, articles, tools and service developments direct to your inbox.
Each update helps you stay connected with new and relevant Food Industry Hub content, with links back to resources you may want to read, use or revisit.
Lean Six Sigma for Food Safety and Quality Assurance Improvement
In food manufacturing, two vital goals stand at the forefront: ensuring food safety and maintaining exceptional quality standards. Achieving these objectives is not only essential for regulatory compliance but also for meeting consumer expectations. Lean Six Sigma, a powerful methodology known for process optimisation and error reduction, can be a game-changer when applied to food safety and quality assurance. Here, we will explore how Lean Six Sigma can be harnessed to drive continuous improvement and excellence in the food industry.
Understanding Lean Six Sigma
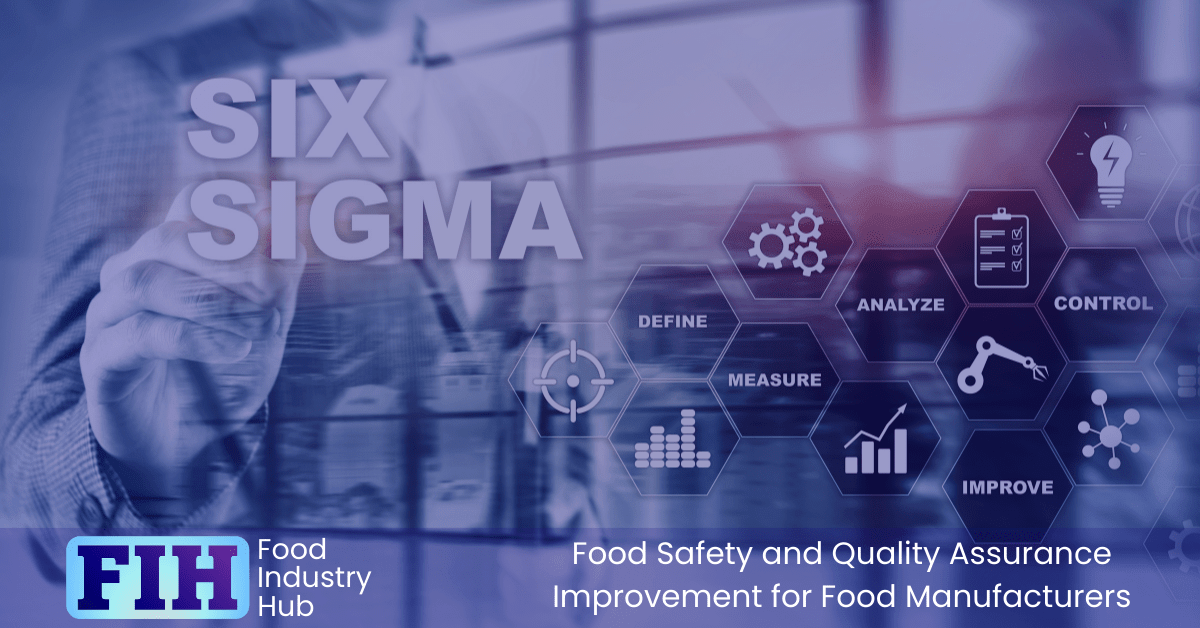
Lean Six Sigma is a structured, data-driven approach that combines the principles of Lean (efficiency and waste reduction) and Six Sigma (process improvement and defect reduction). Its primary objective is to eliminate waste, streamline processes, and reduce variation to enhance overall efficiency and quality. Applying this methodology to food safety and quality assurance brings several benefits:
1. Defining Food Safety and Quality Goals
In the Define phase of Lean Six Sigma, clear objectives are established:
Define Food Safety Standards: Identify specific food safety and quality standards and regulatory requirements that must be met. These become the baseline for improvement efforts.
Set Quality Metrics: Define key quality metrics and performance indicators, such as the number of defects, contamination levels, or adherence to procedures.
Clarify Customer Expectations: Understand consumer expectations and preferences regarding food safety and quality, incorporating these into the objectives.
2. Identifying Waste and Inefficiencies
In the Measure phase, data collection and analysis help identify inefficiencies and waste in food production processes:
Data Collection: Gather data on processes related to food safety and quality, including ingredient handling, production steps, packaging, and storage.
Root Cause Analysis: Determine the root causes of quality issues, safety concerns, and inefficiencies in the production process. This may include examining factors such as equipment failures, employee errors, or supply chain interruptions.
3. Streamlining Processes
The Analyse phase involves a thorough examination of processes:
Process Mapping: Create detailed process maps to visualise the flow of ingredients and products through various stages of production. Identify bottlenecks and areas where waste occurs.
Improvement Opportunities: Identify opportunities for process improvements that will enhance food safety and quality while eliminating waste.
4. Implementing Solutions
The Improve phase focuses on implementing solutions:
Solution Development: Develop and test potential solutions to address identified issues. This may involve process changes, equipment upgrades, or employee training.
Pilot Testing: Conduct pilot tests to evaluate the effectiveness of proposed solutions before full-scale implementation.
5. Monitoring and Control
In the Control phase, measures are put in place to sustain improvements:
Standardisation: Ensure that successful changes are standardised into the production process, and standard operating procedures (SOPs) are updated accordingly.
Continuous Monitoring: Establish a system for continuous monitoring of key quality and safety metrics to detect deviations early.
Benefits of Lean Six Sigma in Food Safety and Quality Assurance
Reduction in Errors and Contamination: Lean Six Sigma’s focus on process improvement leads to a significant reduction in errors and contamination risks, enhancing food safety.
Efficiency Gains: By eliminating waste and optimising processes, food manufacturers can operate more efficiently, reducing costs and lead times.
Consistency in Quality: Streamlined processes and error reduction lead to greater consistency in product quality – meeting or exceeding consumer expectations.
Regulatory Compliance: Lean Six Sigma aids in meeting and maintaining regulatory compliance by ensuring that processes consistently adhere to safety standards.
Customer Satisfaction: Higher product quality and safety enhance consumer trust and satisfaction, leading to increased brand loyalty.
Data-Driven Decision-Making: The methodology’s emphasis on data enables data-driven decision-making and proactive problem-solving.
Lean Six Sigma is a formidable approach that empowers food manufacturers to elevate their food safety and quality assurance practices. By systematically applying Lean Six Sigma principles, businesses can optimise processes, reduce errors, and ensure that every product meets or exceeds safety and quality standards. In an industry where consumer trust is paramount, Lean Six Sigma is the key to providing safe and top-quality food products that stand out in the marketplace. Embrace Lean Six Sigma as your partner in achieving excellence in food safety and quality assurance, and watch your reputation and success flourish.
Kaizen For Food Safety and Quality Assurance Improvement
Many businesses are turning to Kaizen—a Japanese philosophy of continuous improvement – as a methodology for continuous improvement.
Understanding Kaizen in Food Safety and Quality Assurance
Kaizen, which means “change for the better” or “continuous improvement” in Japanese, is a methodology that centres on making small, incremental improvements in processes, products, and services. When applied to food safety and quality assurance, Kaizen takes on specific characteristics:
1. Continuous Improvement Culture
Kaizen fosters a culture of continuous improvement within food manufacturing organisations:
Incremental Progress: Kaizen encourages businesses to make incremental, ongoing improvements in food safety and quality assurance. These improvements can be as simple as optimising a cleaning procedure or refining a quality control process.
Regular Feedback: It promotes the collection of feedback and suggestions from employees at all levels. In the context of food safety, this could mean involving frontline workers in identifying potential hazards and proposing solutions.
2. Waste Reduction
Kaizen is particularly effective in identifying and eliminating waste (known as “Muda” in Japanese) in food production processes:
Process Streamlining: It prompts organisations to scrutinise their processes to pinpoint unnecessary steps, reduce wait times, and eliminate bottlenecks.
Resource Optimisation: By minimising waste, Kaizen helps food manufacturers optimise their use of resources, including raw materials and energy, leading to cost savings.
3. Employee Involvement
One of Kaizen’s core principles is active employee involvement:
Cross-Functional Teams: Cross-functional teams can be formed to address specific food safety or quality issues. These teams are empowered to identify problems, propose solutions, and implement changes.
Training and Empowerment: Employees are trained and empowered to contribute to the improvement process. This not only enhances food safety and quality but also boosts employee morale and engagement.
4. Data-Driven Decisions
Kaizen relies on data and facts to guide decision-making:
Data Collection: In the context of food safety and quality assurance, Kaizen encourages the collection and analysis of data related to process performance, product quality, and safety compliance.
Root Cause Analysis: When issues arise, Kaizen promotes thorough root cause analysis to identify the underlying reasons for problems. This enables organisations to address the root causes rather than merely treating symptoms.
5. Small, Manageable Steps
Kaizen advocates making small, manageable changes:
Risk Mitigation: In food safety, this approach minimises the risk associated with implementing significant process changes, ensuring that product safety is not compromised.
Resistance Reduction: Smaller, incremental changes are often met with less resistance from employees, making them more likely to embrace and sustain improvements.
Benefits of Kaizen in Food Safety and Quality Assurance
Enhanced Food Safety: By continuously identifying and addressing potential hazards and risks, Kaizen improves food safety practices, reducing the likelihood of contamination and foodborne illnesses.
Consistent Quality: Through process optimisation and waste reduction, Kaizen ensures consistent product quality.
Cost Savings: By minimising waste and optimising resource utilisation, Kaizen can lead to significant cost savings.
Regulatory Compliance: Continuous improvement aligns processes with regulatory standards, reducing the risk of enforcement measures and/or recalls.
Employee Engagement: Involving employees in the improvement process not only leads to better results but also fosters a sense of ownership and pride among staff.
Kaizen is not just a methodology; it’s a cultural shift that can lead to significant improvements in food safety and quality assurance. By embracing the principles of Kaizen and fostering a culture of continuous improvement, food businesses can safeguard consumer health, enhance product quality, and ultimately build trust in their brands. Kaizen in food safety and quality assurance isn’t just about incremental changes; it’s about the continuous pursuit of excellence—one small step at a time.
The Benefits of Improving Food Safety and Quality Assurance Systems
It’s clear that there are major advantages to food safety and quality assurance systems, but it can be useful to be specific about some of the reasons that well-implemented food safety and quality assurance systems can bring valuable benefits.
Consumer Trust and Loyalty – When consumers purchase food products, they place immense trust in manufacturers to deliver safe and high-quality items. Improving food safety and quality assurance systems strengthens that trust. It assures consumers that the products they purchase will consistently meet or exceed their expectations, leading to brand loyalty and repeat business.
Regulatory Compliance – Regulatory bodies worldwide enforce stringent standards and regulations to safeguard public health. Enhancing food safety and quality assurance systems ensures compliance with these standards. Compliance not only helps avoid costly fines and legal consequences but also demonstrates a commitment to ethical and responsible food production.
Reduced Product Recalls and Liability – Product recalls can be financially devastating and damage a brand’s reputation irreparably. By improving safety and quality assurance systems, manufacturers can reduce the likelihood of defects, contamination, or non-compliance issues that lead to recalls. This not only saves money but also mitigates the risk of legal liability.
Cost Savings – Improving food safety and quality assurance often involves streamlining processes and reducing waste. These efficiencies lead to cost savings in areas such as resource utilisation, energy consumption, and labour. Over time, these cost savings can significantly improve a manufacturer’s bottom line.
Competitive Advantage – Consumers are increasingly discerning about the food they consume. Manufacturers with robust food safety and quality assurance systems gain a competitive edge by offering products that meet or exceed industry standards. This advantage can lead to increased market share and brand differentiation.
Enhanced Reputation – A positive reputation is invaluable in the food industry. Manufacturers with a reputation for producing safe, high-quality products not only retain their existing customer base but also attract new customers who prioritise safety and quality. Reputation is often the deciding factor for consumers choosing between similar products.
Improved Supply Chain Relationships – Manufacturers depend on a network of suppliers to source raw materials and ingredients. Improving food safety and quality assurance systems can lead to better relationships with suppliers. Suppliers are more likely to meet higher standards when working with manufacturers who prioritise safety and quality.
Customer Satisfaction – Quality assurance systems ensure that products consistently meet or exceed predefined quality standards. When customers receive products that consistently meet their expectations, they are more likely to be satisfied and loyal, leading to positive word-of-mouth marketing and repeat business. An alternative way of thinking about this would be that improved quality assurance should result in a reduction in customer complaints.
Risk Mitigation – Enhancing food safety and quality assurance systems helps identify and mitigate potential risks early in the production process. This proactive approach minimises the chances of food safety incidents, quality issues, or product recalls.
Long-Term Sustainability – A commitment to improving food safety and quality assurance systems promotes long-term sustainability. By reducing waste, conserving resources, and minimising risks, manufacturers contribute to a more sustainable and responsible food industry.
Conclusion
Improving food safety and quality assurance systems isn’t just about meeting regulatory requirements; it’s about exceeding consumer expectations and ensuring the long-term success and reputation of food manufacturers. The benefits of these improvements, including consumer trust, regulatory compliance, cost savings, and competitive advantage, make it a worthy investment for any food manufacturer committed to excellence and responsibility.
In Summary
Circumstances evolve all the time, and it’s impossible to be prepared for every scenario that may present itself. Ask risk factors and technologies develop, so must approaches to food safety and quality assurance.
The approaches outlined here are intended to prepare you with a mental framework for approaching continuous improvement and problem-solving as you take steps for food safety and quality assurance optimisation.
Further Resources
Food Industry Hub serves the food industry with a range of digital resources for the benefit of both commercial food manufacturers and food industry professionals.
For food manufacturers, we offer integrated management systems that give every user a direct interface with your QMS.
For food industry professionals, we provide an extensive signposting service in addition to informational content we hope you’ll find useful as you face new professional challenges. We have very ambitious plans to expand the range of services offered, and currently present informational content on management, safety and quality, and professional success.


